
Blog List
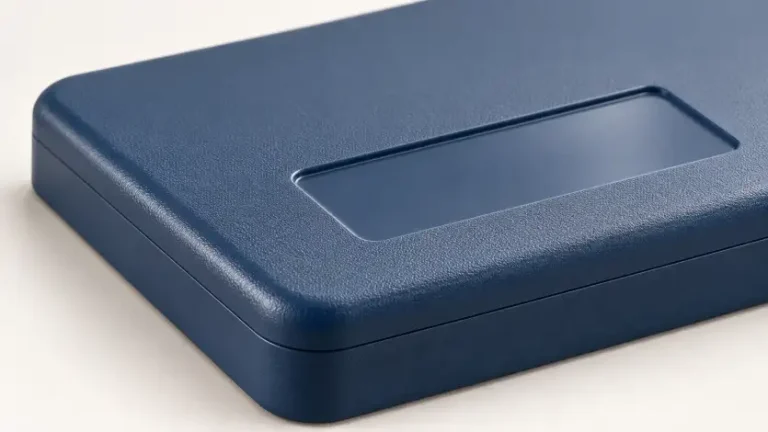
Injection Molding Surface Finish: Beyond the SPI Grade
A molded enclosure may need a textured grip, a smooth label recess, and an untextured mating rim. A general note…
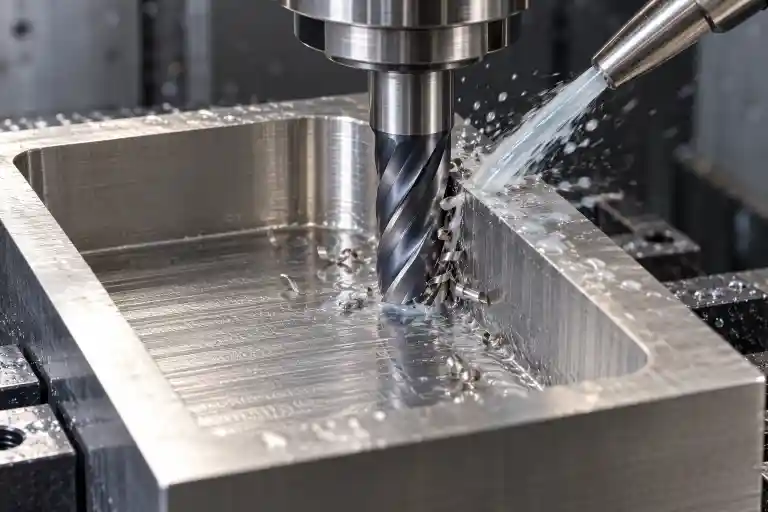
Titanium CNC Machining: Heat, Chip Load, and Thin Walls
Titanium CNC machining requires control of heat at the cutting edge while maintaining a chip thick enough for the tool…
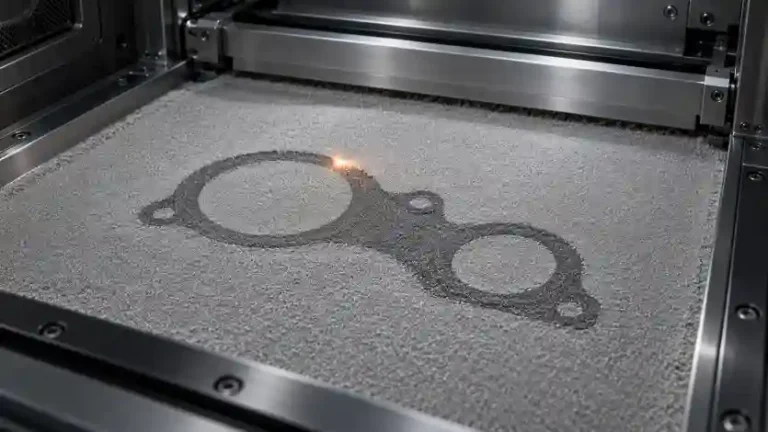
DMLS vs SLM: Compare the Metal, Build, and Finish
Two metal-printing quotes can use different process names and still describe the same broad manufacturing method. They can also use…
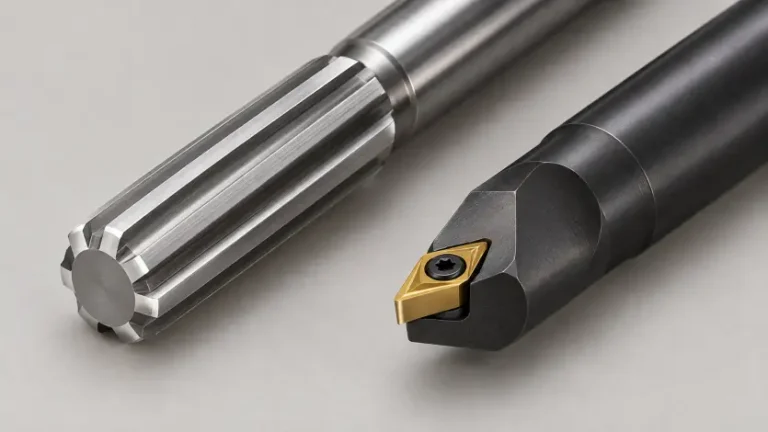
Reaming vs Boring: Choose from the Starting Hole
Reaming and boring both enlarge an existing hole, but they give the machinist different control over the result. Reaming is…
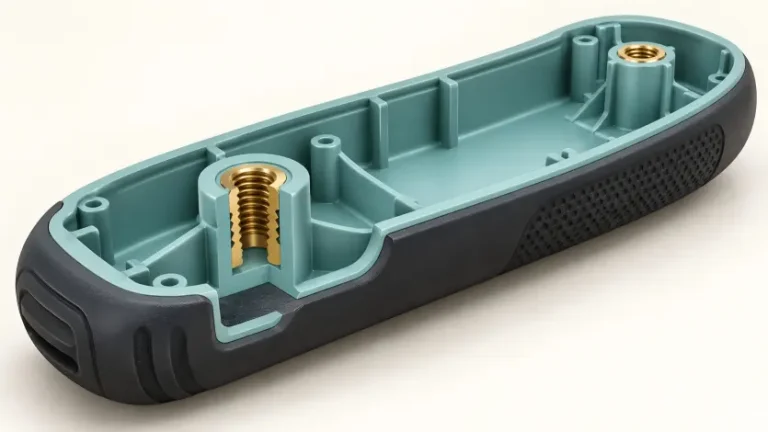
Overmolding vs Insert Molding: Bonds, Inserts, and Tooling
A plastic housing may need a soft grip, metal mounting threads, or both. These features introduce different requirements: the grip…
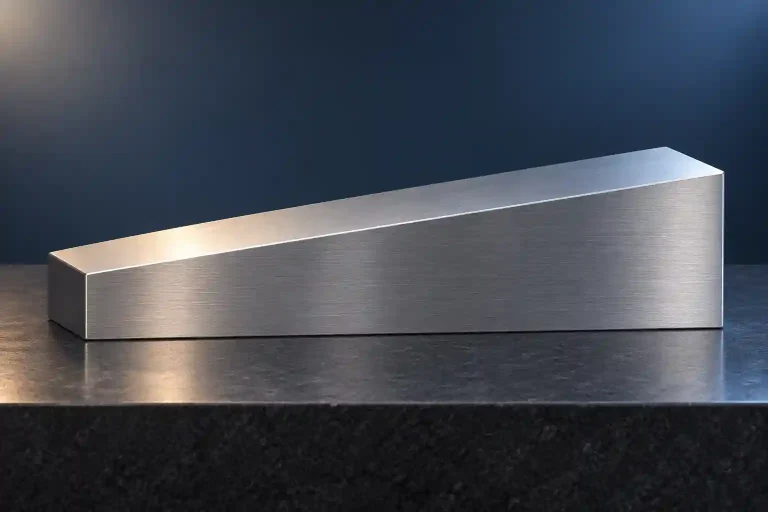
Flatness vs Parallelism: Why a Flat Face Can Still Fail
A machined mounting face can pass a flatness check and still put the mating part at the wrong angle. The…
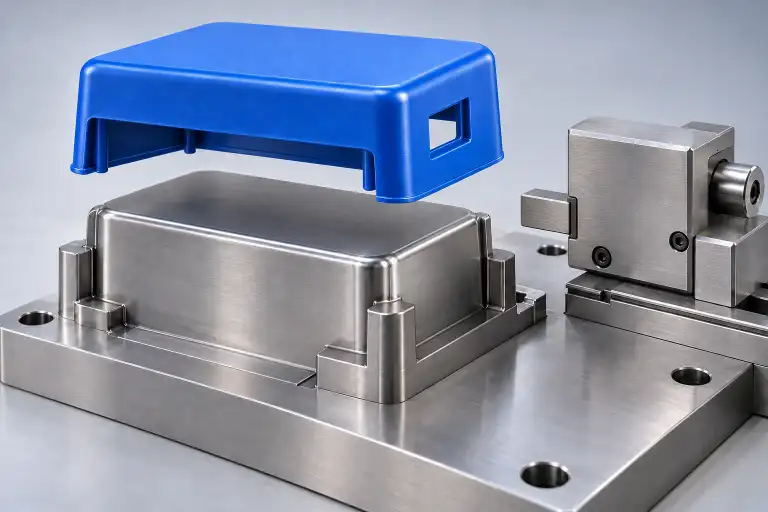
Undercuts in Injection Molding: Plan the Release Path
A snap hook, retaining groove, or side hole can keep a molded part trapped on the steel that formed it.…
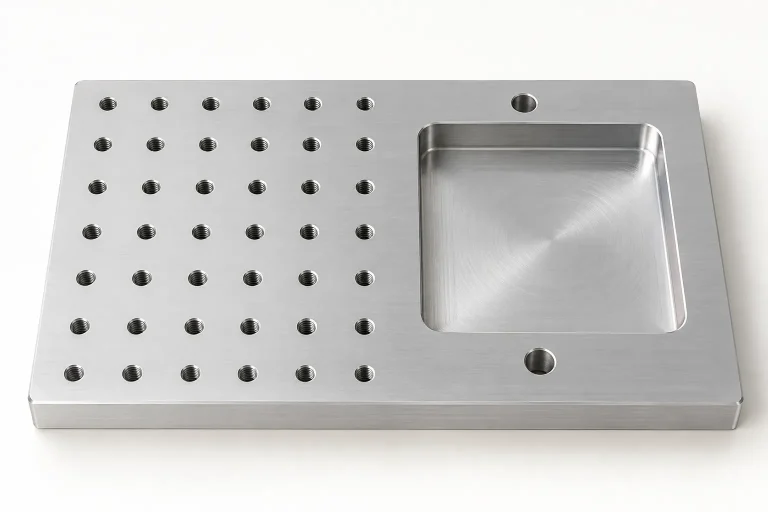
MIC-6 vs 6061 Aluminum: Choose the Right Plate
An aluminum fixture plate can arrive flat, move after pocket machining, or bend when a clamp is tightened. These problems…
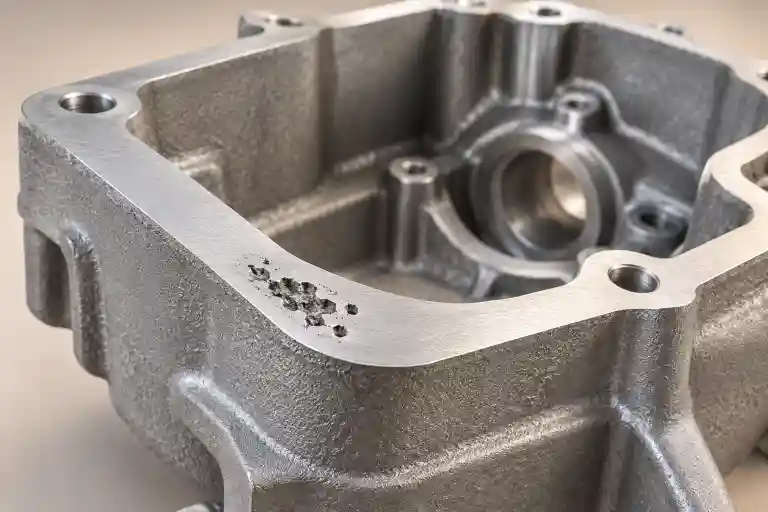
Casting Shrinkage: Allowance, Porosity, and Machining Stock
A cast housing can meet its outside dimensions and still reveal pores when its sealing face is machined. Another casting…